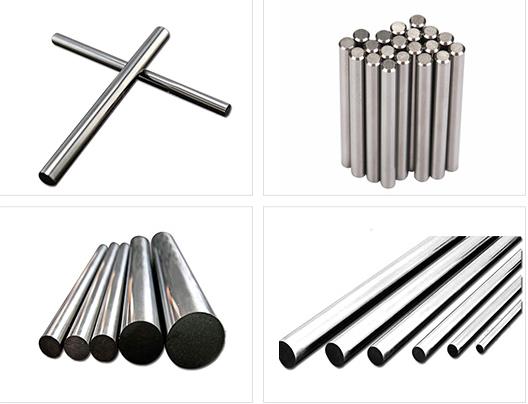
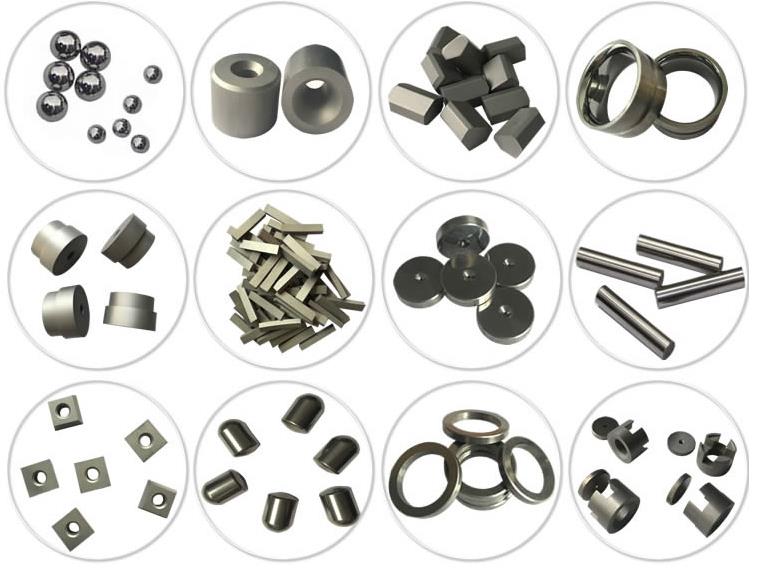
XYMJ has more than 20 years of experience in researching and manufacturing tungsten carbide products such as carbide wire drawing dies, carbide plates & strips, tungsten carbide mining tips, carbide buttons, carbide circular blade and other much more customized tungsten carbide wear parts. XYMJ manufactures tungsten carbide rods with 100% virgin material, advanced sintering furnaces, high-precision grind machines, high stability and high performance guaranteed.
Advantages of XYMJ tungsten carbide rod
1. It adopts high-quality ultra-fine tungsten carbide and imported cobalt powder as raw materials.
.
2. Standardized production technology using the advanced low-pressure sintering technique.
3. It has high strength and high hardness.
4. It has excellent red hardness, good wear resistance, high elastic modulus, high bending strength, superior chemical stability with high resistance of acid, alkali, high-temperature oxidation, superb impact resistance, low expansion coefficient.
5. It is manufactured with high-tech precision advanced equipment which is a low-pressure sintering furnace.
6. It is produced by a unique new process with the vacuum high temperature and high-pressure sintering. The pressure sintering is adopted at the finish time, which greatly reduces the porosity, improves the density and the mechanical properties of the product.
7. carbide rod has many material grades, which can adapt to different applications with complete specifications and precious carbide blank size which can reduce processing volume and improve productivity.
Tungsten carbide rod has the advantages of good HRC, high strength, excellent wear resistance, high chemical stability, etc, which is one of the preferred materials of the drill, end mills and milling cutters, widely used in various machining industries. XYMJ is one of the most trustworthy carbide rod manufacturers, with premium quality products, various types, high-precision equipment and competitive prices.
Tungsten carbide rod, also called carbide round bar, is the preferred material for metal cutting tool manufacturing, widely used in the industries which has high requirements for wear-resistance, corrosion-resistance and high-temperature resistance. It has a lot of outstanding performance.
Tungsten carbide rod, as named as cemented carbide rod, is a high-hardness, high-strength and high-hardness material which has a major raw material of WC, with other metals and paste phases using powder metallurgical methods through low-pressure sintering.
Applications
Carbide rod is mainly suitable for drill, end mills and milling cutters, widely used for cutting, stamping and measuring tools, such as the micro-drill of the PCB industry, the electrode rod of the photoelectric communication, tungsten steel drill bit, drill handle, push rod, precision wear-resistance parts of the mechanical processing industry. It is the best material for the CNC milling cutter and machining cutter with hole.
carbide rod mainly is applied to the precision cutting of non-ferrous metals, YG6X and YG10X which are submicron grain grade, fiberglass reinforced plastic, titanium alloy, YG8X which is ultra-hard steel fine grain grade.
The Categories Of Tungsten Carbide Rod
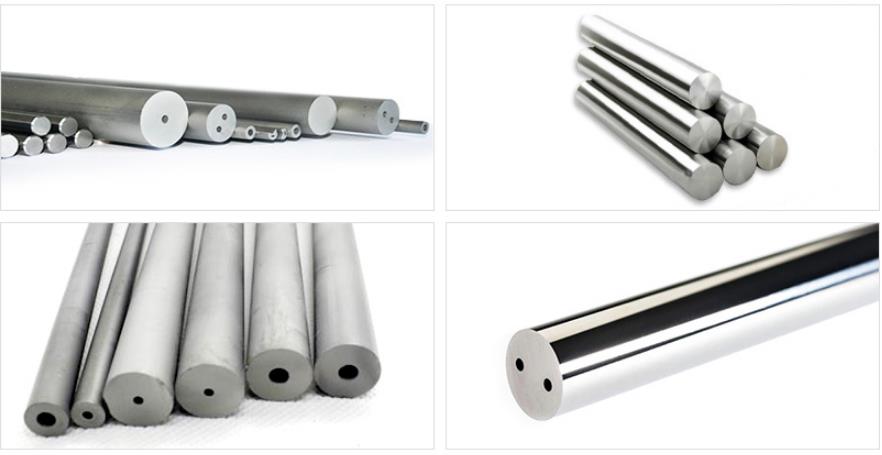
Tungsten carbide rod with straight holes is available, including one, two, three holes, which has a spiral straight line with 30 degrees or 40 degrees or twisted. carbide rods also has the type of non-hole.
According to the structure, a tungsten carbide rod can be classified into a PCB tool, a solid tungsten carbide bar, a single straight-hole bar, double straight-hole bar, a two-spiral bar, three-spiral bar, and other types.
According to the molding process, carbide rods can be classified into two types of extrusion molding and compression molding. The difference is that the extrusion carbide rod and bars have a beautiful appearance, easy for grinding processing. The advantage of the molded bar is that the density is relatively uniform, but it is not conducive for grinding processing.
In most cases, cemented carbide products will have a good surface finish, allowing machining with super fast speed, much higher than high-speed steel and other tool steel, bearing higher temperature. Cemented carbide tool will have superior cutting performance with excellent wear resistance.
1. Cutting tool material
Cemented carbide adopted as the cutting tool material, is the widest application. Among the carbide tools, the tungsten cobalt carbide is suitable for the cutting of black metal, non-ferrous metals and processing of non-metallic materials, such as cast iron, cast brass, colloidal wood, etc. Cemented tungsten titanium cobalt is applied for steel and other black metals processing. In the same kind, there is more cobalt content, suitable for rough machining and less cobalt content is used for fine machining. Universal cemented carbide has a much longer service life than that of stainless steel which is difficult for processing.
2. Mould material
Cemented carbide is mainly used for cold wire drawing dies, cold punching dies, cold extrusion mode, cold heading dies and other cold stamping molds.
Under the wear-resistant working conditions which have a strong impact, the tungsten carbide cold heading mould is required to have a good impact toughness, fracture toughness, fatigue strength, bend intensity and excellent wear resistance. Usually, among grades of high cobalt and medium, crude granules, the YG15C is commonly adopted.
In general, the relationship between the carbide wear resistance and carbide toughness is contradictory. The increase in wear resistance will result in a decrease in toughness and the increase in toughness will inevitably lead to a decrease in wear resistance. Therefore, when choosing a cemented grade, it is necessary to meet specific usage requirements based on the processing objects and processing conditions.
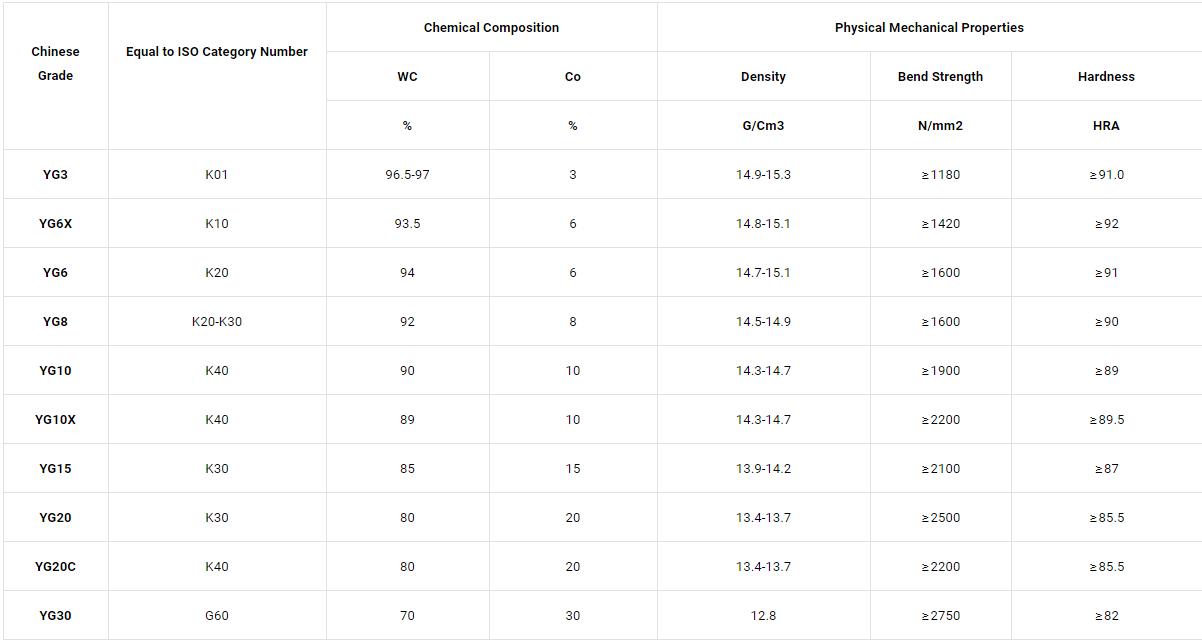
If the selected grade is easy to occur early cracks, it is advisable to use a grade with high toughness. if the selected grades is easily damaged due to the early wear, it is appropriate to choose a grade with a higher hardness and better wear resistance. The following grades of YG15C, YG18C, YG20C, YL60, YG22C, YG25C have a gradual decrease in hardness and wear resistance and gradually improving toughness.
3. Measuring tools and wear parts
The cemented carbide is adopted in the wear surface inlay and parts of the measuring tools, precision bearing manufactured by grinding machine and the Cemented carbide wear parts such as guide bar, lathe center, valve seat.
Cemented carbide is a composite, the main components of which consists of the powder of refractory carbide like tungsten carbide, titanium carbide through the binder metal powder such as cobalt, nickel, etc. It is a cemented composite obtained through the powder metallurgical method. It is mainly used to make high-speed cutting tools for hard, tough materials, cold working dies, measuring tools, high resistant parts with high stability and free from vibration.
The hardness of the cemented carbide at normal temperature can reach HRA of 86 to 93, equivalent to HRC of 69 to 81. High hardness can be maintained at 900 to 1000 ° C with excellent wear resistance. Compared to high-speed steel, the cutting speed can be 4 to 7 times higher with 5 to 80 times longer life. The hard material of 50 HRC can be cut through carbide products.
In addition to the high hardness, wear-resistance cemented carbide has a series of high performance such as good toughness, heat resistance, high corrosion resistance, high elastic modulus, etc, which can be widely used as cutting tool materials, such as turning tool, milling cutter, planner tool, drill bit, etc., suitable for cutting cast iron, non-ferrous metals, plastic, chemical fiber, graphite, glass, stone, ordinary steel, heat-resistant steel, stainless steel, high manganese steel, tool steel and other much more difficult materials. Tungsten carbide wear parts, mechanical parts and carbide wire drawing dies have advantages of high resistance of high-temperature, friction, corrosion. In various industrial applications, tungsten carbide is an ideal choice for replacing steel.
Grades Of Cemented Carbide
YG6, YG6X, YG8
Wear resistance, high strength, suitable for under ordinary stress conditions, manufacturing for cemented carbide ball. It can be used for forming tools, carbide nozzle, spool, valve seat, rotary burrs, seal ring, measuring tools, fixture, mechanical part accessories, etc.
YG11C, YG11
Excellent wear resistance, good impact resistance, used for high voltage nozzle, lining, bushing in the industries of oil, chemical, machinery.
YG15, YG15C
High strength and toughness, applied for under large stress, manufacturing for seal ring, different shaped structural parts, mechanical accessories and stamping dies.
Y20 YG20C
The type of tungsten carbide is suitable for standard parts, bearings, tools and cold heading, cold stamping mould.
Solventless lamination machine has fast speed and high efficiency but also means having high risks in the absence of deviations in process conditions. The most difficult factor is the lag phenomenon of composite materials quality performance. Therefore, the composite process is also known as a special process, how to minimize the risk of solvent-free composite?
1.The Necessary Small Process Sample
Changes in raw materials and process conditions, which will lead to the quality problems of the batch. For example, formulating film material, printing ink type, type adhesive, and so on. At present, the raw material quality of different suppliers is uneven. It is not easy to replace each other, moreover, film materials, ink, adhesives, process conditions, still matched, such as solvent-less.
For example, -oh which is now widely used in the polyurethane ink resin, consumes a certain amount of rubber curing agent and the degree of consumption is related to the ratio of the ink layer and the thickness of the resin in the ink layer. The adhesive layer of the ink layer portion does not appear.
After the sample test has been passed, technical documents should be formulated in strict accordance with the established process and the raw material supplier will provide a stable formulation. If the raw material formulation or process conditions have changed, the sample should be re-tested.
2. Comprehensive Quality Inspection
For quality inspection, it should focus on the composite film appearance, peel strength, heat sealing strength, heat sealing temperature, solvent residue, At the same time, food packaging, pharmaceutical packaging is different in terms of sample treatment, soaking method, soaking conditions (time/temperature), indicator units.
Today, food packaging safety is widely concerned that the safety test of packaging materials is also one of the important factors of reducing business risks.
3.Solvent-free Composite Technology
The maximum characteristics of solventless composite technology, materials for solvent-free composite and drying composite, are low initial viscosity, small coating. Various quality problems have occurred primarily related to these two factors. Therefore, the experience gained through dry composite methods can’t be simply transplanted into a solventless composite.
For example, when the glue flow at both ends of the gluing baffle is insufficient, it is easy to aging, resulting in reduced glue and insufficient peel strength at both ends of the composite film with the uneven glue. The side of the baffle should be stirred regularly.
At the same time, it is necessary to ensure the correctness of the ratio of the two-component binder and the curing agent. The metering pump blocking can result in a ratio error of the two-component gels and the curing agent, For example, a batch accident in which the curing agent is insufficient, resulting in insufficient dryness of the composite film, less than the peel strength and low heat sealing strength. So correctly detecting the refractive index of the rubber, monitoring the accuracy of the ratio, avoiding the situations, which including maintenance that cannot be maintained, the unbalanced binder proportion and no alarm for mixing pump, are necessary for improving solventless composite technology.
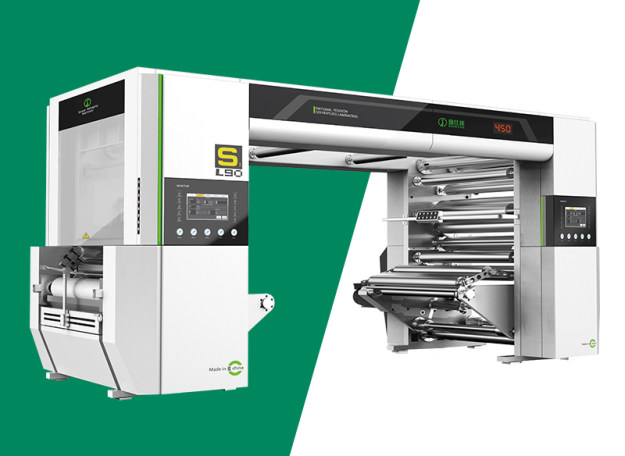
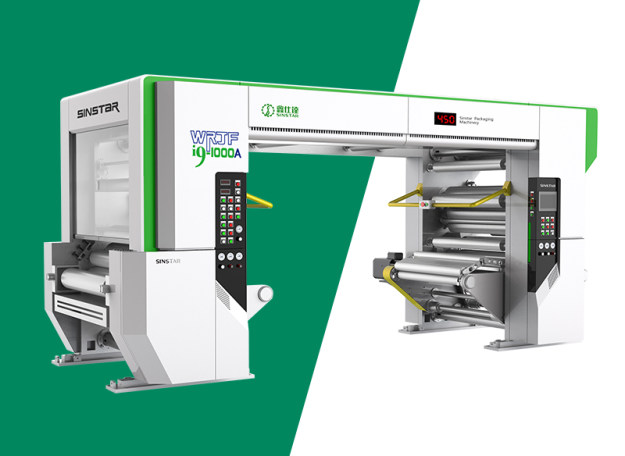
The solventless lamination is more and more widely used in the flexible packaging industry with the advantages of high efficiency, low cost and environmental friendly. Learning how to reduce the bulk loss and minimize the risk of solventless composite can greatly do a favor for the better operation of a solventless laminator.
Solvent-free composite technology is mainly adopted for solventless lamination machines. Significant advantages of the solventless composite process are reducing cost, high efficiency and energy saving, improving production safety, stability and product quality.
However, due to the immature solventless composite technology , and there are still some technical risks that are easily overlooked in the application for a flexible packaging company, leading to quality problems. Now we summarize three common risk control points of solvent-free composite technology.
1. The Technical Risk Of Increasing A Glue In Solventless Composite
Solvent-free composite adhesive with A glue and B glue, the adhesive mixing ratio is generally the weight ratio of A glue and B glue, rather than the volume ratio of both. The mixing ratio of the binder is usually determined by the adhesive manufacturer, as the proportion of the binder in different brands is generally different. The common ratios of A glue and B glue are 100: 80,100: 75,100: 50,100: 45. However, in the actual solvent-free composite production of flexible packaging companies, the ratio of the two-component adhesive will be disordered, which will affect the solventless quality of flexible packaging products.
Case
After printing, solvent-free compounding, the flexible structure of OPP / VMPET / PE has no quality problems.
The structural composite flexible bag is a low viscosity-free solvent-free binder brand and the proportion of A glue and B glue in actual composite production is 100: 67. When analyzing the cause of failure, we find that the bag is curled and the inner binder is not dry. Originally, because the composite film maturity is incomplete, prolongs the maturation time and then cuts into a bag. The problem of bag curling still exists and the opening performance has also deteriorated.
Combined with a ratio of A glue and B glue, it is not difficult to find that the bag is mainly caused by the excess of the A glue, because the solvent-free composite film is usually large and the effect of prolonging maturity is not obvious, water must be introduced into the cross-linking curing reaction with the -NCO.
The much more efficient methods are to rewind the composite film roll on a slitting machine and then increase the humidity of the workshop environment to absorb some moisture between the layer and the surface. The composite film, during aging, water will penetrate into the adhesive layer and reacted with an excess-NCO cross-linking curing reaction, so that the self-adhesive layer will be further completely cured, thereby effectively release the curling of the flexible packaging bags.
2. Risk Control For The Attenuation Of PE Membrane Peel Strength At Solventless Composite Material
A certain amount of linker is added to the film blow molding for reducing the friction between the film and the film, the film and the device, so that the surface of the film will be smoother, in order that the composite film operates successfully in the production process. Under normal circumstances, an excess sliding agent has added appropriately in the PE film, which can solve the phenomenon of abnormal increase in the friction coefficient of the solvent composite film after a certain extent, but this can also cause peel strength to be weakened, which is serious. When the aging is completed, the peel strength of the composite film is exceeded and in most cases, the peeling strength is reduced during the process of placing the composite film or during the cycle of the flexible packaging.
Case
The composite structure is a BOPA / PE film
Main parameters: a brand solvent-free adhesive, the amount of glue is 1.5 g / m2, aged at 40 ° C for 24 hours. The tracking and detection data of the peel strength of the composite film is as follows:
On October 13, the lateral peel strength was 15.37 N / m.
On November 4, the lateral peel strength was 4.62 N / m.
After the complex layer is peeled off, the surface of the PE film has a mist-like substance that can be wiped off.
On November 18, the lateral peel strength was 4.69 N / m.
It is closed to the final test data indicating that the peel strength of the composite film has reached a stable value.
Typically, the flexible packaging company only detects the peel strength of the composite film shortly after maturity. The composite film is rarely tracked during the process or the peel strength in the soft bag, which should be noted.
The migration of the solventless adhesive in the PE film produces a slipping agent, which is the main reason for the decrease in the peel strength of the composite film. We recommend a solvent-free adhesive. Add the formulated slipping agent to the formulation, so that the friction coefficient of the PE film in the solvent-free compound can be solved, and the problem of decrease in peel strength can also be solved.
3. Pay Attention To Identifying The Smell Characteristics Of The Solventless Adhesive
There are many factors that produce scent in the flexible packaging bag, such as residual solvent, ink resin, thin-film raw material resin, adhesive, etc. Although there is no solvent residue in a solventless composite, the resins and formulations in the solventless adhesive have a certain odor feature and some have effects after composite curing, even after the packaging. For flexible packaging companies, it is necessary to pay attention to the identification of the solventless composite film after the smell and prevent the problem.
a. In GB / T 10004-2008 standard, the detection method of packaging sensory indicators is specified, which is opening the box and lining the packaging film and immediately detect the smell.
b. Usually take a certain area of the composite films, cut into a 500 ml glass bottle, baked for 30 minutes at 60-80 ° C for detecting smell. It is also possible to seal the package in the air or actual content, rotating at a temperature of 50 to 60 ° C, tearing the package, and feel whether there is odor.
The odor of the composite film is mainly from a solvent-free adhesive. Therefore, the odor feature of the general solventless adhesive can be identified by the following method.
a. Take a certain amount of A glue and B glue with different brands for sensory testing and comparison.
b. Add a mixed solvent-free binder according to the specification to the glass bottle. Plastic film is placed in the bottom of the bottle and the cured adhesive is easily taken out and the crosslinking reaction is under 40-50 ° C. After an hour, the odor characteristics are determined. This method is more suitable for practical applications, including the odor characteristics of the resin itself.
Solvent-free composite technology is a production technology which is more and more widely used in the flexible packaging industry with the advantages of safety, environmental protection, saving costs. Through the learning of the common risk control points of solventless composite technology, the efficiency of solventless lamination will be improved.
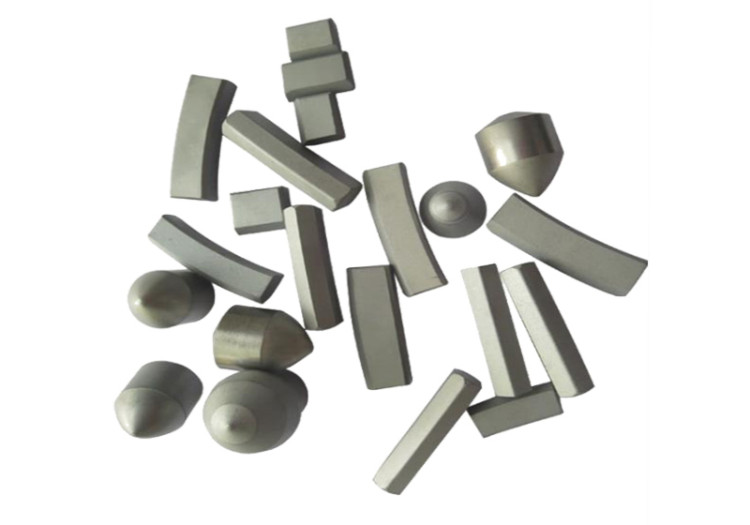
Tungsten carbide plays an extremely important role in the machining process because it offers higher wear resistance than high-speed steel, which can withstand higher working temperatures and can be very well optimized to meet the requirements of various processes. It can meet high demands for the performance of cutting tools. According to the shapes of customized tungsten carbide cutting tools, the carbide cutting tools are classified into round blades, ring blades, long blades, arc blades, toothed blades, trapezoidal blades, wave blades, serrated blades, disc blades, and special-shaped blades, etc.
Advantages Of Tungsten Carbide Cutting Tools
1.Improved durability and wear-life, up to 600% better than standard steels.
2.Greater productivity and less down time due to fewer blade changes.
3.Cleaner and more precise cuts due to reduced friction.
4.Reduction in start-up and end of line waste.
5.Better overall cutting performance in high heat and high speed cutting environments.
Tungsten Carbide Rotary Burr
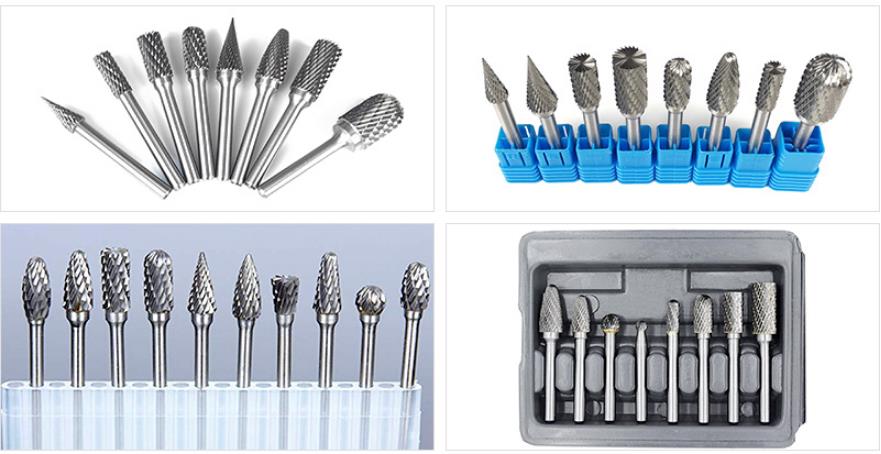
Tungsten carbide rotary burrs have been used widely in the shipping construction, auto engine porting and foundry fabrication. With its high rotating speed and hardness, it can machine a lot of different materials, such as cast iron, carbon steel, alloy steel and non ferrous material. High life service of product is warranted for virgin and excellent raw material which is one of most critical factors to the carbide burr’s life.
Carbide rotary burrs can be applied with both electrically-powered and pneumatically-powered hand-held tools to cut various types of materials including aluminum, brass, titanium alloys, cast iron, copper, etc. They can be widely used for pneumatic, electric drive tools.
Various Types Of Materials Can Be Cut With Tungsten Carbide Burrs
Aluminium
Brass
Titanium alloys
Cast Iron
Copper
Zinc alloys
Types of alloy steel
Bronze
Various plastics
Nickel
Stainless steel
Tungsten Carbide Brazed Tips
Tungsten carbide brazed tips can be used for drilling soft rock formations under F=8, hard and supper hard coal formations, natural stone materials, bricks and concrete walls. For special applications, specific materials can be adapted to satisfy customers’ requirements. XYMJ can supply various types of tungsten carbide brazed tips including A type, B type, C type, D type, E type, K type, etc.
Tungsten Carbide Circular Blade
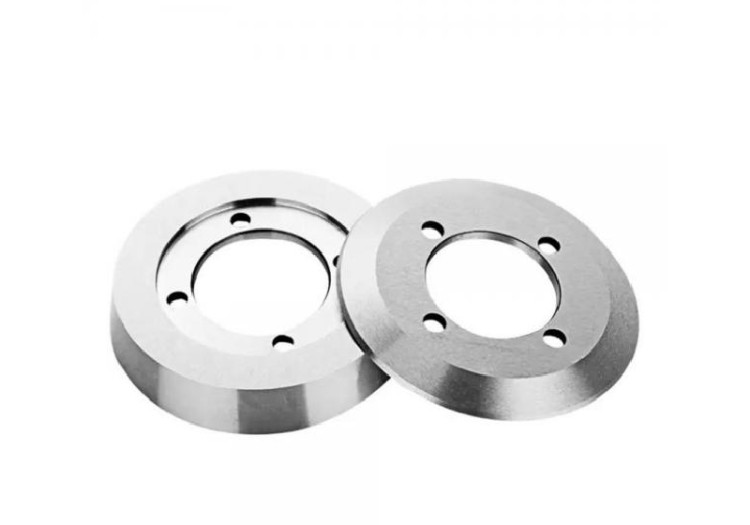
Tungsten carbide circular blade can be applicable to various industries and fields ,the products are widely used in ceramics, printing machinery, paper, carton, paper tube, forestry, plastic machinery, food machinery, textile, electronics, light industry, aluminum foil copper foil, metal film, tobacco, cigarette materials, packaging materials, BOOP film, edge sealing, seal, bottom sealing machine, wood processing, food packaging, wire and cable, steel smelting, shipbuilding, chemical, textile, plastics, leather, plastic crushing industry and other industries.
Features
(1) Less knife consumption costs.
(2) Strictly quality control for excellent valve.
(3) High precision, high intensity.
(4) Excellent hardness,small thermal deformation.
(5) Matched to their applications.
(6) Reduce unsurpassed edge quality.
(7) Increased blade durablity and reduced retooling time.
(8) Excellent cutting quality,stable and reliable cutting performance.
All of the tungsten carbide mining tools provided by XYMJ are made from virgin raw materials with advanced technology for high precison grinding and polishing. Various sizes and styles are available with custom service.
Tungsten Carbide Buttons</p
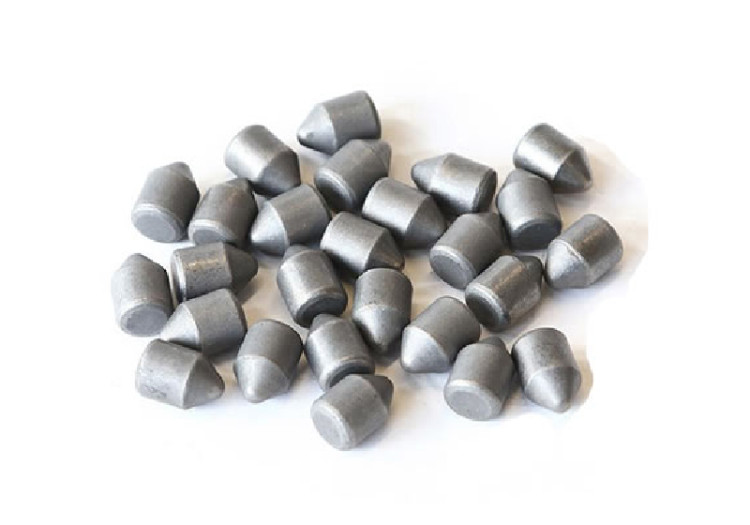
XYMJ provides the drill bit of carbide mining buttons with passivating treatment for a 5 to 6 times longer service life than the same diameter of drill bit, which saves much time and manual labor, different types available, including type B, type E, type P, type Q, type S, type Z, etc.
Features
1.high strength and high hardness.
2.excellent hardness, wear-resistance, high elastic modulus, high flexural strength.
3.good chemical stability (acid, alkali, high-temperature oxidation), impact resistance.
4.good toughness, low coefficient of expansion, etc.
Tungsten Carbide Mining Tips
Tungsten carbide tips are widely used in oilfield drilling and snowplow, or other equipment because of their unique properties, mainly including tips for road milling, tips for coal mining, tips for tunneling and tips for trenching, etc. In a word, tungsten carbide mining tips are used for rock cutting and milling with big consumption. Stability and high technology ensure the high quality of XYMJ carbide mining tips.
Mainly material grades include YG4C, YG8, YG11C, YG15. YG8 material grades are used for coring crowns, electrical coal drill bits, coal cutting picks used in geological prospecting, coal mining. YG11C grades are used for heavy rock drills and rotary hammer rock drills cutting hard rocks. YG15 grade has a high intension, lower wear resistance. Suitable for making bits for rotary machine and heavy rotary machine to drill hard and very hard rock.
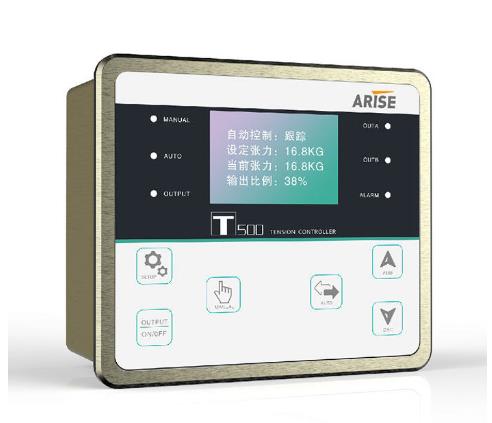
The tension controller is a high-precision instrument with digital, automatic control for web tension. It can be widely used in tension control of the printing, packaging, paper, textile and dyeing industries. Web tension controller adopts the CPU of 16-bit or 32-bit, with high speed, high precision, high reliability.
Why Choose The Automatic Tension Controller
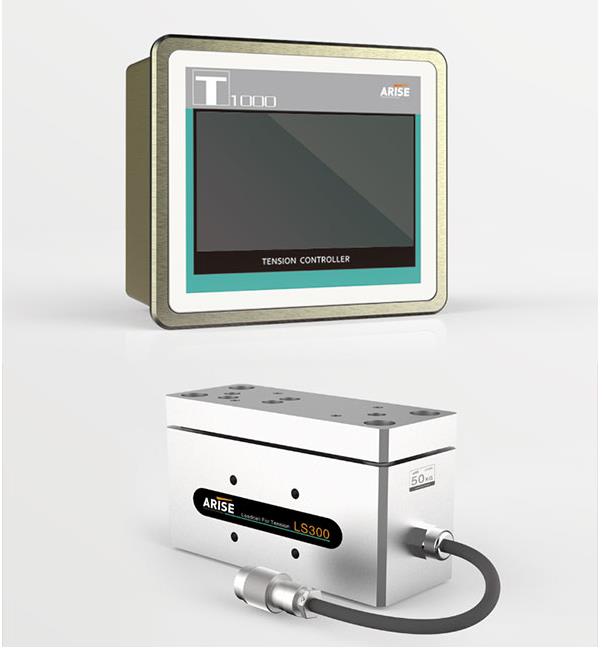
A typical tension control system is mainly composed of a tension controller, a tension reader, a tension sensor, a magnetic powder brake, and a clutch. Depending on the loop, it can be divided into types of open loop, closed loop or free ring. According to the monitoring method of different coils, it can be divided into types of ultrasonic, floating roller, tracking arm. The stability of tension control has directly affected the quality of the slitting products. If the tension is insufficient, it will generate drift in the raw materials moving and the finished paper wrinkle will appear after the rewinding. If the tension is large, the raw material is easily broken, so that the finished products will appear more broken ends after the rewinding.
The Performance Of The Automatic Tension Controller
The tension controller refers to the durable control of the tension performance when the feedstock is stored on the device. This control is required to be valid for any operating speed of the machine, including the deceleration, acceleration, and uniform speed of the machine. Even in emergency parking conditions, it should be guaranteed that the parties are not damaged.
The automatic tension controller is a control instrument that can directly set the tension value of the controlled machine, then directly output the signal of the tension sensor as a tension feedback value, after the proposed bias, outputting to the PID controller for disposal. Then input to the core executive agency to control and finally arrives the purpose of a small bias.
Function Of The Automatic Tension Controller For Unwinding And Rewinding
In the control industry, in some strip-shaped and line-shaped products, tension control is required to achieve production requirements. The general tension controller also has a volume extent function, which is generally applied to the down coiler equipment, with unwinding and winding types. The tension controller also has a taper adjustment function that can be sent directly to the winding taper on some processes inside the controller.
Fully automatic tension control is the actual tension value of the material, measured by the tension sensor directly, and then converts the tension value into a tension signal feedback to the tension controller. Through the comparison of this signal and the pre-set tension value, calculates the control signal. The automatic control execution unit makes the tension value is equal to the pre-set tension value, to achieve a stable purpose for tension control. A fully automatic tension controller is an advanced tension control method.
The fully automatic tension controller measures the actual tension of the coil materials and automatically adjusts the tension value of the coil according to pre-set tension value through the PID algorithm. It has extremely high accuracy tension control, suitable for applications where have high requirements for the accuracy of the tension controller.
How To Solve The Malfunction Of The Automatic Tension Controller
1. The automatic tension controller adopts the AC 185-264V power supply. After the current is switched on, if the tension controller does not work, check if the power supply is connected correctly or whether the fuse is abnormal.
2.If the display signal is incorrect, can re-set the correct signal range. Check the route and the tension sensor whether there is a signal fault or replace the tension sensor.
3.If the tension controller has no signal output, usually there is a connection problem, so check whether the signal output connection is correct, then turn off the voltage for ten seconds and then switch on.
4.If the tension controller signal output is unstable, check whether the roller, bearing and magnetic powder clutch, brake, or driver have an abnormality. Replace the tension sensor or re-calibrate the signal range.
Once there is not an alignment of the coils, it will cause errors in the subsequent steps and the material wasting or the downtime of the machine. Therefore, when processing the web, the web guiding is necessary for the offset and it is widely used in a bonding machine, a printing machine, a coater, a paper machine, a dyeing machine, etc, which has various requirements for the winding and rewinding processes. An all-in-one web guiding system refers to the technical operation of the coils to keep the edge of the coil neat and consistent during spraying, printing, die-cutting, lamination, slitting, or other coil winding processes. Its wide applications have brought huge benefits to the coil industries. The all-in-one system has automated industries such as corrugated paper, textile, printing, labels, papermaking, plastic film, building materials, tires, and non-woven corrugated paper processing.
The Work Principle Of All-in-one Web Guiding System
The high-precision, high-speed, and high-efficiency coil automatic processing has high requirements for the lateral position of the controlled coil. Equipped with a high-performance automatic web guide system is the key to improving coil production capacity and output. The coil will shift laterally during moving, unwinding and rewinding. Therefore, the web guiding system can be installed in the above three positions for controlling the coil to pass through the designated position accurately.
All-in-one web guide machine adopts high-speed microprocessor, digital, modular and intelligent circuit design. The advanced programming, user-friendly interface, high-performance components and complete circuit protection design, make the system run continuously and stably. The response time of the control system is less than 0.01 seconds and the accuracy of the system itself can reach 0.01mm. During the coil winding process, the web guide sensor detects the position of the edge or line to pick up the deviation signal of the edge or line position.
Then the position deviation signal of the web guiding machine is sent to the web guide controller for logical operation. After the judges and processes of the control unit, it will control the drive motor to skew the web to the correct position.
The Functions & Advantages Of All-in-one Web Guiding System
The high-performance web guide system has a fast response time, high-speed CPU calculation and can support ultrasonic sensors, photoelectric sensors, CCD sensors for the different response of coils. It has the advantages of simple and practical operation, ball screw, high precision, low noise, maintenance-free, long service life, flexible installation.
Center compensation deviation web guiding can quickly guide the high-frequency feed errors. It integrates operation and control technology with a highly compact web guide. The guiding system has an innovative sensor detection real-time display and a real-time feedback system for system detection information.
The all-in-one system is driven by a brushless DC servo motor and precision ball screw, with compact structure, good mechanical rigidity, low inertia, high precision, suitable for high-speed and high-precision web guide in coil processing.
Three Detection Methods Provided By All-in-one Web Guiding System
The All-in-one web guiding system provides three different detection methods, which include edge detection, line tracking, or alignment detection. The drive system is driven by a brushless motor and the drive stroke is strictly proportional to the coil offset. The system can also be used in conjunction with different sensors to meet the needs of different coils, such as ultrasonic sensors, photoelectric sensors, CCD sensors, etc. The microcomputer digital controller provides precise control for the various functions of the guide system.
Daily Maintenance Of All-in-one Web Guiding System
1.Alignment: Tools, workpieces and accessories should be placed neatly. The web guiding system should be equipped with thorough protection equipment.
2. Cleaning: Cleaning inside and outside including all sliding surfaces, guidelines, gears, racks, etc, ensuring all parts will not leak oil, water, air, or electricity.
3. Lubricating: Refuel and change oil timely. The oil quality meets the requirements. Oil tanks, oil guns, oil cups, lumps, tubes should clean and keep complete.
4.Safety: The operation personnel should be familiar with the maintenance structure of the web guide system, complying with the operating procedures and reasonably use the all-in-one system with daily maintenance, carefully maintenance tools to prevent accidents.