4 Tips to Know Drilling and Well Control Simulators Quickly

Drilling and well control operations play a crucial role in the oil and gas industry, demanding skilled professionals and specialized equipment to ensure safety, efficiency, and productivity. As these activities grow increasingly complex, the importance of effective training and education cannot be overstated. In response to this need, drilling and well control simulators have emerged as powerful tools in the industry. This article explores the key features, benefits, challenges, and future prospects of these simulators, highlighting their role in improving safety and minimizing environmental risks.

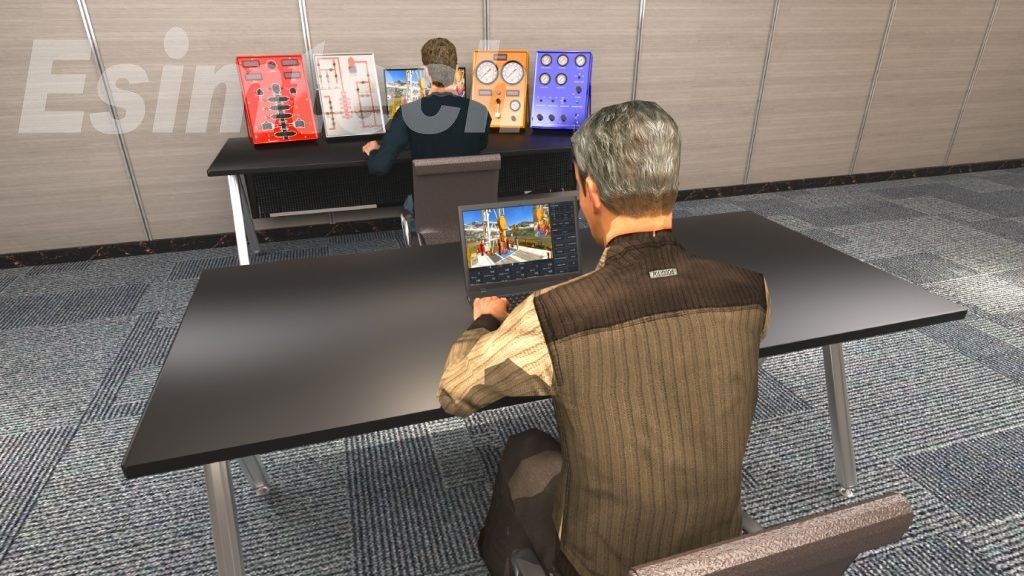
Cyberchair Drilling Simulator

Understanding Drilling and Well Control Simulators

Drilling and well control simulators are computer-based systems that recreate real-world drilling and well control operations within a simulated environment. They offer a realistic and interactive training experience, enabling operators to practice and refine their skills and knowledge in a safe and controlled setting. Simulators come in various types, including drilling simulators, well control simulators, and combined drilling and well control simulators.

How Do Drilling and Well Control Simulators Work?

Drilling and well control simulators consist of software and hardware components. The simulation software employs mathematical models to replicate the physical and mechanical aspects of drilling and well control operations. On the other hand, the hardware components comprise control panels, joysticks, and other equipment that facilitate user interaction with the simulator. Operators can input different parameters and scenarios, receiving output data and analysis in return.

Benefits of Using Drilling and Well Control Simulators for Training and Education

Drilling and well control simulators offer numerous advantages for training and education, including:

Safety and Risk Reduction: Simulators provide a safe environment for operators to develop their skills and knowledge without the inherent risks of real-world operations.

Cost-effectiveness and Efficiency: Simulators offer a cost-effective and efficient training method, eliminating the need for expensive equipment and resources required in real-world scenarios.

Realistic and Interactive Training Experience: Simulators provide an immersive training experience that closely replicates real-world operations, enabling operators to enhance their skills and knowledge effectively.
Customizable and Scalable Training Programs: Simulators allow for tailored and scalable training programs that can be adapted to meet the specific needs of operators, operations, and organizations.

Differences Between Simulators and Real-World Operations

While drilling and well control simulators provide significant benefits, it’s essential to recognize the disparities between simulators and real-world operations. Simulators have inherent limitations and challenges that can impact their accuracy and realism. To ensure operators are fully prepared for actual operations, real-world experience should complement simulator training.
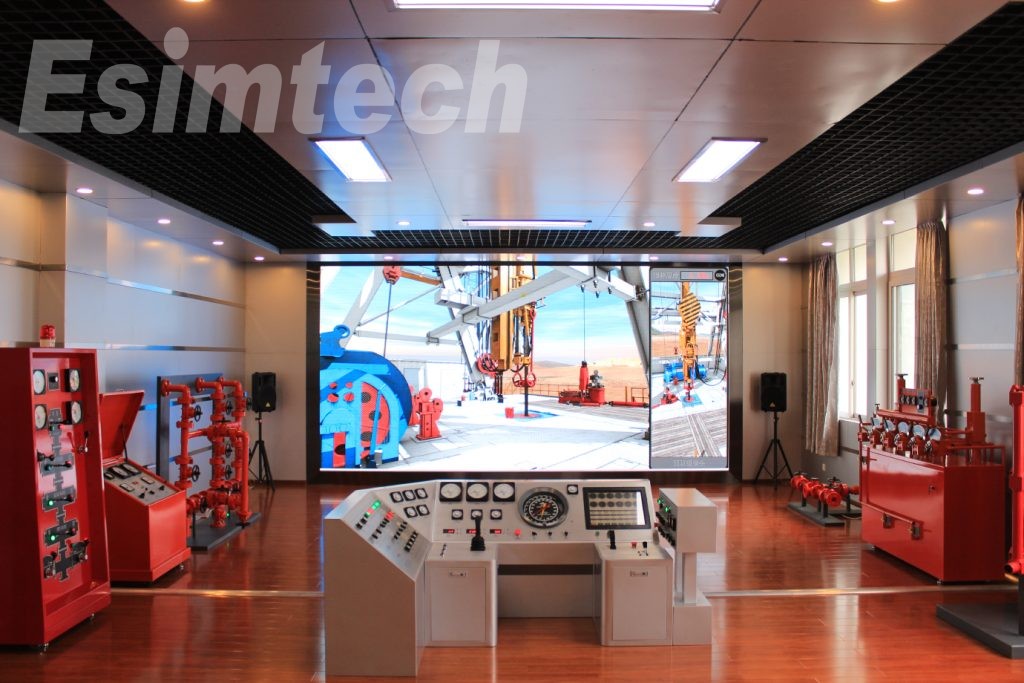
drilling and well control simulator

Challenges and Limitations of Drilling and Well Control Simulators

The accuracy and complexity of simulation models, accessibility of simulators, and the associated costs and maintenance are some of the challenges and limitations facing drilling and well control simulators. Addressing these challenges is crucial to ensure simulators remain effective and efficient as training and education tools.

Future Developments and Innovations

The future and innovations of drilling and well control simulators holds promising advancements. Anticipated developments include improvements in simulation technology, integration with artificial intelligence and machine learning, and expanded use of virtual reality and immersive training techniques. These innovations will enhance the accuracy and realism of simulators, delivering an even more engaging and lifelike training experience for operators.

In summary, drilling and well control simulators have revolutionized training and education in the oil and gas industry. Their realistic and interactive nature, coupled with their potential for customization and scalability, makes them invaluable tools for ensuring safety, efficiency, and expertise in drilling and well control operations. With ongoing advancements and innovation, simulators will continue to play a crucial role in preparing operators for the challenges of the industry while reducing risks and environmental impact.
What are Commonly Used Incubators

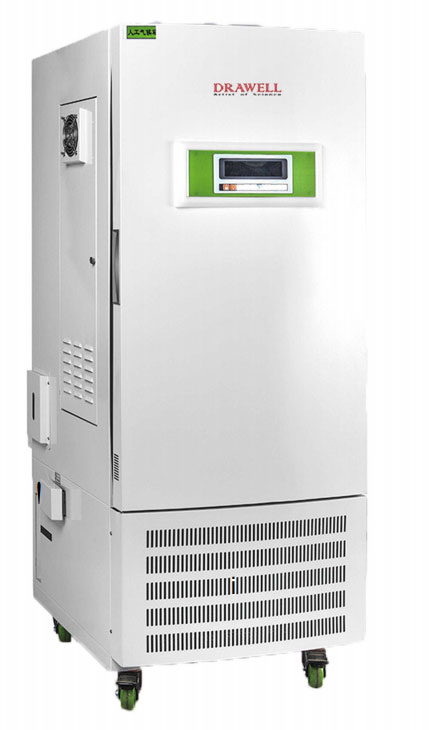
Incubators are commonly used laboratory instruments that provide controlled environments for the growth of cells, tissues, microorganisms, and other biological samples. There are several types of incubators available, each designed for specific applications. In this article, we will explore the commonly used incubators, their features, and their uses.

drawell incubator

Constant Temperature Incubators:

Constant temperature incubators maintain a steady temperature throughout the incubation process. They are widely used in various fields such as plant biology, microbiology, genetics, and medicine. These incubators simulate specific temperature conditions required for the growth and development of cells, tissues, and organisms.

Constant Temperature and Humidity Incubators:

Constant temperature and humidity incubators, as the name suggests, provide precise control over both temperature and humidity. They are commonly used in experiments and research involving sensitive biological samples that require specific humidity levels in addition to temperature control. These incubators find applications in fields like environmental testing, culture testing, and more.

Carbon Dioxide Incubators:

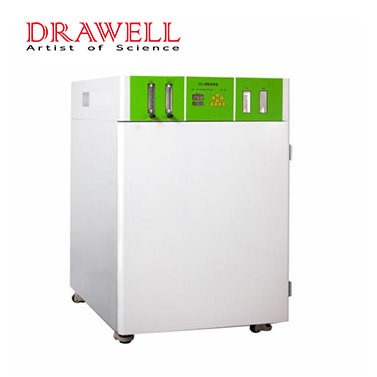
Carbon dioxide (CO2) incubators create an environment similar to that found in living organisms, particularly for cell and tissue culture. They regulate temperature, CO2 levels, and pH to support the growth and viability of cells. CO2 incubators are extensively used in cell biology, tissue engineering, drug screening, and other related research fields.

CO2 incubator

Anaerobic Incubators:

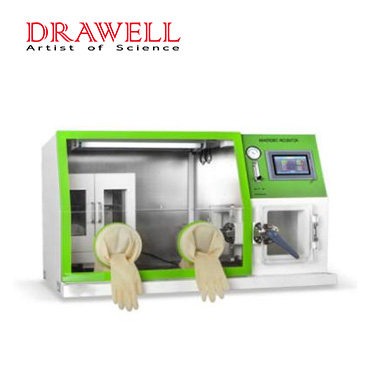
Anaerobic incubator, also known as anaerobic workstations or anaerobic glove boxes, provide a controlled environment devoid of oxygen for bacterial culture and experimentation. These incubators create strict anaerobic conditions, allowing the cultivation of anaerobic organisms that cannot survive in the presence of oxygen. They are essential tools for anaerobic biological detection and scientific research.

anaerobic Incubator

Mold Incubators:

Mold incubators are specifically designed for the cultivation of eukaryotic microorganisms such as molds. They typically maintain room temperature and a specific humidity level to support mold growth on solid substrates. Mold incubators feature refrigeration systems, heating systems, air humidifiers, control circuits, and operation panels to regulate temperature and humidity inside the incubation chamber.

Each type of incubator has distinct features and applications. It is important to select the appropriate incubator based on the specific requirements of the experiment or research being conducted. Additionally, proper use and maintenance of incubators are crucial to ensure accurate and reliable results.

In conclusion, the various types of incubators, including constant temperature, constant temperature and humidity, carbon dioxide, anaerobic, and mold incubators, offer researchers and scientists the ability to create controlled environments to support a wide range of biological studies and experiments. Understanding the differences and capabilities of these incubators will enable users to choose the most suitable option for their specific needs.

5 Key Points to Know Stockless Anchors

Stockless anchors are gaining popularity in marine applications due to their versatility and compact design. These anchors, suitable for small boats and large ships alike, offer a range of advantages for various seabed conditions. In this article, we will explore on the topic of what are stockless anchors, including the definition, design components, types, installation, maintenance, and the advantages and disadvantages of stockless anchors.

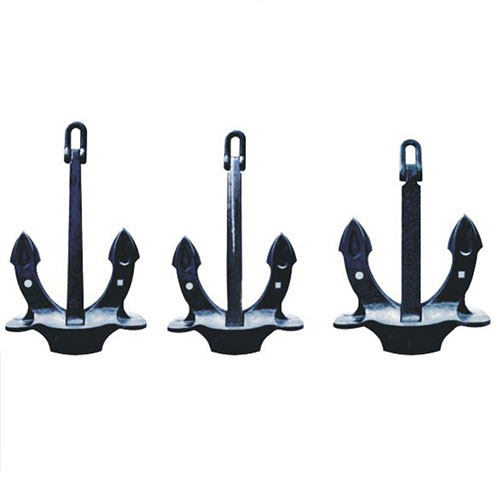
hall anchor

Definition of Stockless Anchors:

A stockless anchor is a type of marine anchor that lacks a vertical bar called a stock, which assists in proper pivoting and setting on the seafloor. Instead, the shank of a stockless anchor is directly attached to the anchor chain or rope. This design allows the anchor to rotate and dig into the seafloor without the need for a stock. Stockless anchors are popular due to their small size, ease of use, and ability to provide reliable holding power in various seabed conditions.

Design and Components of Stockless Anchors:

While the design and components of stockless anchors may vary depending on the manufacturer and intended purpose, they typically consist of the following parts:

Shank: The shank serves as the anchor’s main body, providing the necessary weight and structure to keep the anchor in place. It features a bent or fluked end that aids in digging into the seafloor.

Flukes: Flukes are the flat, curved, or pointed sections of the anchor that dig into the seafloor, providing gripping power. They can be shaped like a scoop or a wing and vary in number, size, and angle based on the anchor’s size and type.

Crown: The crown is the top part of the anchor, typically featuring a hole or slot for attaching the anchor chain or rope.

Tripping Ring: A small ring attached to the crown, the tripping ring is used in emergencies to remove the anchor from the seabed.

Chain or Rope: The anchor chain or rope connects the anchor to the boat, supplying the necessary tension to keep the anchor in place. A shackle is often used to secure it to the anchor’s crown.

Various Types of Stockless Anchors:

Stockless anchors come in different types, each suited for specific marine applications and seabed conditions. Some common types include:

AC-14 Anchor: This anchor offers excellent dragging resistance and holding force, commonly found on offshore oil rigs and large marine vessels.

Hall Anchor: Lightweight and compact, the Hall anchor is ideal for smaller vessels, providing good holding power in soft to moderate seabed conditions.

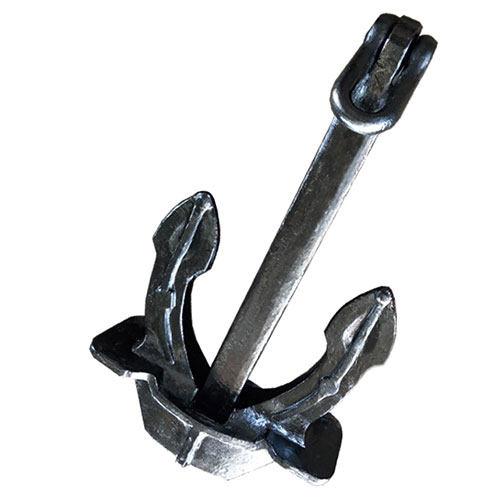
Spek Anchor: Designed for challenging seabed conditions like rocks, the Spek anchor is a heavy-duty option frequently used on large ships and offshore rigs.

spek anchor

Pool Anchor: Pool anchors are versatile and adaptable, suitable for a variety of bottom conditions such as mud, sand, and rock. They are commonly seen on small to medium-sized ships.

Baldt Anchor: With high-strength capabilities, Baldt anchors are used in heavy-duty marine applications like oil rigs and large cargo ships.

Delta Anchor: Popular among recreational boats and smaller commercial vessels, the Delta anchor offers strong holding ability across different seabed situations.

Installation and Maintenance of Stockless Anchors:

Proper installation and maintenance are crucial for the optimal performance and longevity of stockless anchors. Follow these guidelines for installation and maintenance:

Installation:

Before installation, inspect the chain or rope for any damage such as fraying, rust, or wear and tear. Replace any damaged components before proceeding.

Ensure the anchor is appropriate for the size and weight of the vessel and the seabed conditions. Follow the manufacturer’s instructions regarding chain or rope lengths.

Lower the anchor carefully and gradually, paying out the chain or rope to avoid damaging the anchor and to ensure proper placement on the seabed.

Verify that the boat is securely fastened in place once the anchor is set.

Maintenance:

After each use, inspect the anchor for any damage or wear, such as bent flukes or cracks in the shank. Rectify any damage or consider replacing the anchor if necessary.

Regularly clean the anchor to prevent corrosion and rust, which can weaken its holding capacity.

Inspect the chain or rope periodically for deterioration, corrosion, or fraying. Replace any damaged sections promptly.

Follow the manufacturer’s instructions for maintenance and inspection intervals, which may vary depending on the material and usage of the anchor.

stockless anchor

Advantages and Disadvantages of Stockless Anchors:

Consider the following advantages and disadvantages when selecting a stockless anchor for your marine application:

Advantages:

Compact design facilitates easier handling and storage.

Easy deployment, especially in shallow waters.

Good holding power on various seabed conditions.

Reduced risk of snagging on underwater debris.

Versatile and suitable for a wide range of vessels.

Disadvantages:

Limited pivoting capability compared to anchors with stocks.

May not perform as effectively in high winds.

Limited holding power in hard seabeds.

May require more frequent maintenance due to compact design.

Higher cost, particularly for high-strength materials.

Summary

Stockless anchors offer a compact and versatile solution for marine applications. Their design, lack of stock, and various components enable ease of use, reliability, and efficient anchoring. By understanding the advantages and disadvantages of stockless anchors, as well as considering specific requirements for each application, you can make an informed decision when selecting the most suitable anchor for your marine needs.

3 Useful Ponints to Know Magnetic Powder Brake

A magnetic powder brake is a device that controls the torque between a motor and a load in an exact and variable manner. It is an essential component in many industries that require accurate torque and tension control. Its durability, versatility, and ease of use make it a desirable solution in a variety of industries.

Magnetic Powder Brake is widely used in a variety of industries.

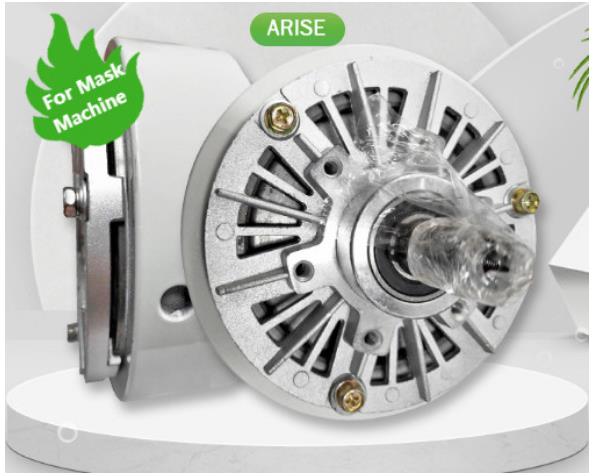
magnetic powder brake

Magnetic powder brakes are useful in these industries because they enable precise and consistent control over torque and tension during the manufacturing process. This is essential for ensuring that the end product satisfies the specifications and is consistently of high quality.

Printing Industry

It is used in printing machines to control the tension of the web or paper during the printing process. This ensures that the printed material is consistently of high quality and devoid of aberrations.

Packaging Industry

It is used to regulate the tension of the packaging material throughout the manufacturing process. This is critical for ensuring that the packaging material is wound correctly and without slippage or wrinkling.

Textile Industry

A magnetic particle brake is used in textile industry to regulate yarn tension during the spinning and weaving operations. This is required to ensure that the yarn is tightly twisted and that the cloth is of uniform quality.

Industrial Equipment

During the manufacturing process, it is utilized to adjust torque and tension in various industrial machinery such as extruders, coaters, and slitters. This is essential for ensuring that the end product is consistently of high quality and meets the required parameters.

How Does a Magnetic Powder Brake Work?

The working of a magnetic powder brake is that the braking force is generated by the interaction of magnetic particles in powder form with the magnetic field created by an electromagnetic coil. A rotor and a stator comprise a magnetic powder brake. The rotor is the output shaft that is connected to the load, whereas the stator is the stationary component that houses the electromagnetic coil. Between the rotor and the stator is a magnetic substance sandwiched. When a current is passed through the electromagnetic coil, it generates a magnetic field that interacts with the magnetic powder, causing the particles to align in the direction of the magnetic field. When the rotor rotates, the magnetic particles are dragged along with it, creating a resistance force in the powder that opposes the rotor’s motion. This resistance force is proportional to the strength of the magnetic field produced by the electromagnetic coil, which is directly proportional to the input current. The rotor’s braking force can be varied by adjusting the input current to the electromagnetic coil. This allows for exact adjustment of the torque supplied from the motor to the load.

magnetic powder brake details

Factors to Consider For Choosing a Magnetic Powder Brake

Output torque requirements

When choosing a magnetic powder brake, the first aspect to consider is the amount of torque required to stop or retain the load. You must select a brake that can provide the necessary torque to ensure that the load is managed safely and correctly.

Speed requirements

The load speed and rotating speed of the brake must be considered while selecting a magnetic powder brake. You must ensure that the brake is designed to perform at the speeds required by your application.

Environmental factors

The environment in which the brake will be used is an important factor. Temperature, humidity, and dust levels can all have an effect on brake performance and lifespan. You must choose a brake that is intended to work in the environmental circumstances of your application.

Power requirements

Magnetic particle powder brakes require electricity to operate, and the power supply must be compatible with the brake. You must ensure that the power supply voltage, frequency, and current are appropriate for the brake.

Size and weight

If space and weight are constraints in your application, the physical size and weight of the brake are critical considerations. If space and weight are significant considerations, a small and lightweight brake should be selected.

Cost

The price of the magnetic powder brake is also an important issue to consider. To obtain the most bang for your buck, you must weigh the cost of the brake against its performance and features.

4 Key Points to Know Cold Extrusion Process for the Production of Fasteners

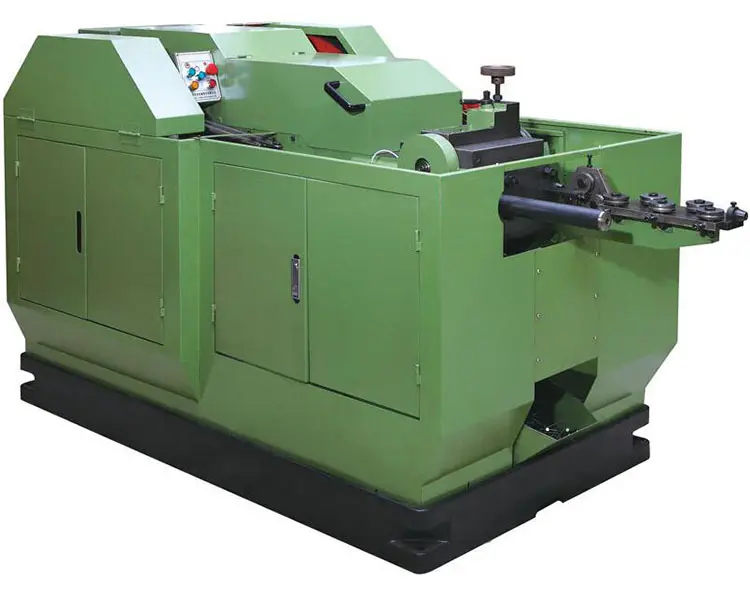
cold extrusion equipment

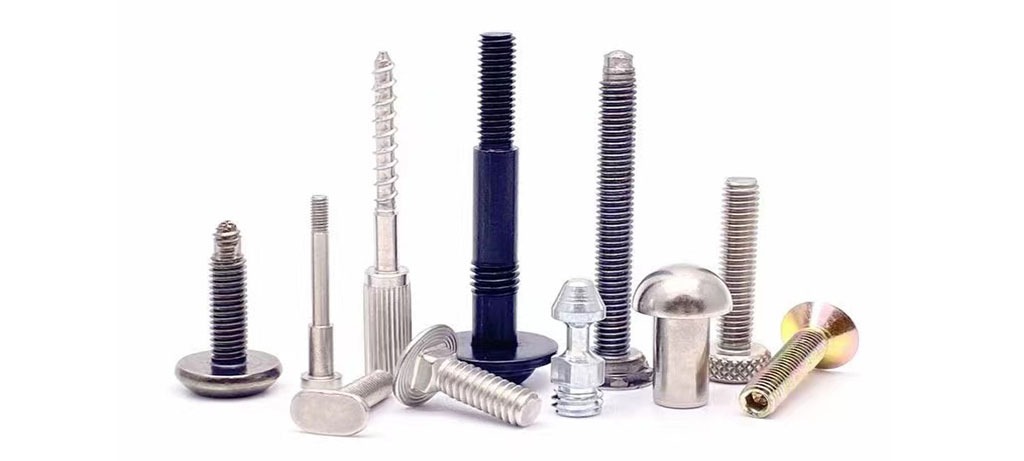
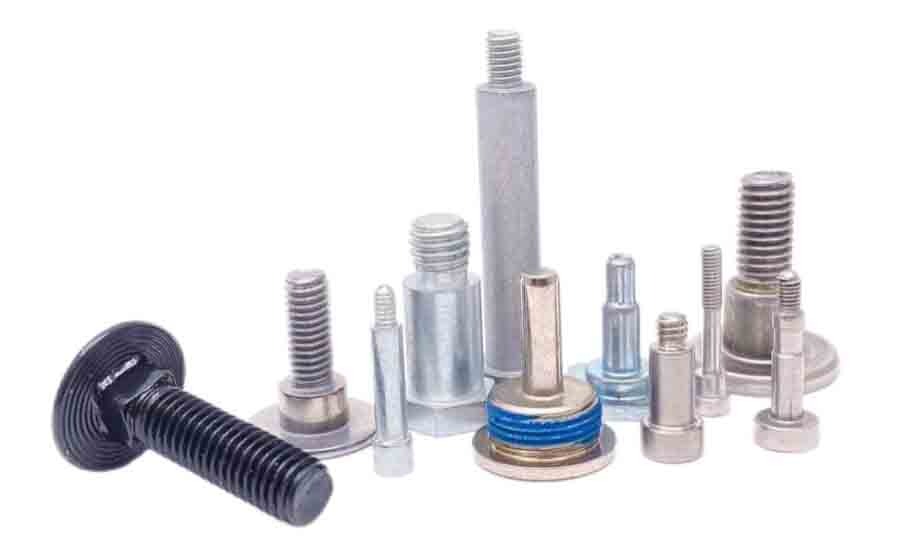
Cold heading is a non-cutting metal pressure processing technology that falls under the topic of metal pressure processing. Cold extrusion process is a key procedure in the manufacturing of fastening pieces. Cold extrusion is the best method for producing bolts, screws, nuts, and rivets.

What is Cold Extrusion

Cold heading is a critical component of precision plastic forming technique. Cold extrusion is the process of inserting a metal blank into a mold cavity while it is still cold. The metal material is forced to form plastic flow under the influence of high pressure and a specific speed in order to obtain the desired shape, size, and some extrusion parts with specific mechanical qualities.

Obviously, the purpose of cold extrusion processing is to control metal flow via molds, and a significant quantity of metal volume is transferred to produce parts. In fact, any fastener can be formed not only by cold heading, but also by a range of deformation methods like as extrusion, punching, and rolling.

fastener supplier

Advantages Of Cold Extrusion

1. Reducing the use of raw materials.

Cold extrusion uses plastic deformation of metal to create the required parts, which reduces the cutting process and increases resource use. Cold extrusion materials can often be utilized at a rate of more than 80%.

2. Improve labor productivity

Manufacturing parts using a cold extrusion technique rather than a cutting process can enhance production several times, if not dozens of times.

3. The pieces have the perfect surface roughness and size precision.

Cold extruded parts rarely require re-cutting and only need to be ground for exceptionally high standards.

4. Improve part mechanical properties

The cold work hardening of metal through cold extrusion processing and a reasonable fiber streamline distribution inside the parts results in a substantially higher strength of the parts than the raw materials. Furthermore, a proper cold extrusion process can create compression stress on the surface of the pieces, increasing fatigue intensity. As a result, some components that require heat treatment enhancement can be saved by using the cold extrusion procedure.

5. Machinable parts with complicated shapes and difficult to cut processing.

Such as irregular section, complex inner cavity and teeth, and invisible inner grooves.

6.Reduce production cost

Because the cold extrusion process has the advantages of saving raw materials, increasing productivity, reducing the amount of cutting processing, and using inferior materials instead of high-quality materials, which can greatly reduce cost.

cold extrusion equipment

Difficulties In Application of Cold Extrusion Technology

1. High requirements for molds

When cold extruding, the deformation resistance of metal blank is significantly increased under the pressure stress in the mold, which makes the stress suffered much larger than the general stamping mold. In addition to high-intensity, the mold also needs sufficient impact toughness and high wear resistance.

2.A large tonnage press machine is required.

Because of the high deformation resistance of the blank during cold extrusion, press machines weighing hundreds or even thousands of tons are required.

3.Only applicable on a large production scale

Because of the high cost of cold extrusion molds, it is often only appropriate to the manufacture of large quantities of parts. The minimum quantity is 50000 pieces.

4. The surface treatment must be done ahead of time.

Surface treatment not only adds procedures and requires a big manufacturing area, but it is also difficult to automate.

5.Inappropriate for high-intensity material processing

6. Part deformation and corrosion resistance reduce

The plasticity and impact toughness of cold extruded parts have become worse, and the residual stress of the parts is large, which will cause parts deformation and produce stress corrosion.

Development Trend of Cold Extrusion Technology

1.As the energy crisis worsens, people will pay more attention to environmental quality, and increased market rivalry will encourage the growth of forging production in the direction of efficiency, high quality, refinement, energy savings, and material savings. As a result, the production of refined forging parts produced by extruding forming and other techniques will compete in the market.

2.The car has evolved in the directions of lightness, fast speed, and stability. Higher requirements for size precision, weight accuracy, and mechanical qualities of forging parts have been proposed, which will encourage the development of refined production technology.

3. Cold extrusion production is still evolving toward specialized and large-scale organizational production.

4. Extrusion machines will become a trend in the future. The refined production development of small and medium-sized forging parts, as well as the application of cold extrusion technology, will drive the development of multi station cold extrusion machines, precision presses, and unique machines designed and constructed for some forged parts.

Summary

Cold extrusion technology is a high-precision, high-efficiency, high-quality, and low-consumption manufacturing technique that is typically used in large-scale production of fastening parts.

Exploring the World of Diablo IV

Diablo IV

Diablo IV’s primary world is a massive open world medieval apocalypse with gnostic mood, blood, gore, and dark comedy. Sanctuary is a location of calamity, degradation, and pain.

1. Open World

Diablo IV is a medieval role-playing game influenced by occult, demonic, and biblical elements rather than standard high fantasy. The globe will be bigger than ever, with regions 10-20 times larger than in previous Diablo games.

2.Regions in Sanctuary and Hell

In the open world, there are five separate, contiguous regions: Fractured Peaks, Scosglen, Dry Steppes, Kehjistan, and Hawezar. We shall also visit the Hell dimension. More regions may be added after the initial launch.

3.Local Events

There are several activities available in the open world. Events range from everyday occurrences, such as the Drowned attacking the coastline, to world boss occurrences, such as Ashava, the Pestilent.

4. Towns and Strongholds

Over 100 settlements of varying sizes, including Towns and Strongholds, are scheduled for deployment. Major towns are the game’s social hubs, where you can find quests, vendors, a waypoint, and other players. You can examine other players, trade with them, or search for a group.

5.Waypoints

Waypoints are back as a quick way to travel long distances.

There is a navigation system in the open world that allows you to mark a location on the map, which will show the shortest route to that destination on the map.

6.Story and Campaign of Diablo IV

Diablo IV is set decades after the events of Diablo III: Reaper of Souls. Malthael’s campaign wiped out 90% of Sanctuary’s people and devastated the world. The Angels have abandoned humanity, and Heaven’s gates are closed.

Lilith (Daughter of Mephisto, Mother of Sanctuary and Humanity) was summoned to Sanctuary by a wicked ritual for which the Triune is accountable after ages in exile.

Why Choose Downhole Operation Simulator for Workover in the Oil and Gas Industry

The oil and gas industry is one of the most important in the world, supplying transportation fuel and energy to industries. However, as oil and gas wells age, their output often decreases, necessitating maintenance or intervention to boost performance. This type of intervention or maintenance is referred to as a “workover” in the oil and gas sector. Workover is the process of increasing or restoring the productivity of an oil or gas well by maintenance, repair, or stimulation activities.

Oil and gas industry rely on advanced technologies such as Downhole Operation Simulator (DOS) software to undertake workover operations. DOS replicates downhole operations, allowing oil and gas engineers to test and optimize interventions before putting them into action in the field. This technology has become a must-have for oil and gas firms, assisting them in lowering the risks, costs, and downtime involved with workover operations.

In this article, we will explain the concept of workover in the oil and gas industry, why workover is required, and the advantages of employing a DOS for workover activities. We will also look at the many sorts of workover procedures and the approaches used to improve their efficiency. The goal of this paper is to provide a comprehensive understanding of workover in the oil and gas industry and the importance of downhole operation simulator for the workover.

Workover Simulator

Overview of Oil and Gas Workover

Workover Definition

Workover in the oil and gas industry refers to the process of performing maintenance, repairs, or stimulation on an existing wellbore in order to increase productivity or restore integrity. Workover operations are typically performed when a well’s production is declining or mechanical difficulties require addressing.

Workover Process

A multitude of steps are involved in the workover process, including well evaluation, design, planning, execution, and evaluation. The well evaluation process entails examining the well’s condition, identifying problems, and selecting the best way to remedy them. The design process entails creating a detailed plan for the workover operation, including the necessary equipment, supplies, and employees. The planning stage entails coordinating and scheduling the operation’s resources. The execution step involves carrying out the workover operation, including the installation of new equipment, repairs, and maintenance. Finally, the evaluation step involves assessing the effectiveness of the workover operation and making any necessary adjustments.

Workover Types

There are three types of workover operations: remedial, completion, and recompletion. Remedial workovers are undertaken to restore the productivity of an existing wellbore that has had mechanical faults or other production challenges. Completion workovers are performed on newly drilled wells to ensure they are ready for production. Recompletion workovers entail modifying the completion design of an existing wellbore in order to increase its productivity.

Challenges of Oil and Gas Workover

Workover Difficulties and Risks

Workover operations can be dangerous and difficult due to a variety of reasons such as wellbore conditions, well pressure, equipment failure, and weather conditions. These factors can enhance the likelihood of an accident, which can result in personnel injury, equipment damage, or even death. Furthermore, workover procedures can be time-consuming and costly, resulting in lower profitability for operators.

Workover Costs and Productivity

Workover operations can be costly, particularly when dealing with complicated challenges that necessitate the use of specialized equipment and expert employees. Workover activities might incur costs such as equipment rental, personnel, and materials and supplies. Effective workover operations, on the other hand, can increase well productivity and extend the life of the well, resulting in higher profitability.

Workover Safety and Quality

Workover operations necessitate a high level of safety and quality control in order to be carried out appropriately and safely. To protect workers and equipment, operators must follow safety norms and standards. Furthermore, quality control methods must be in place to verify that the workover operation is carried out accurately and produces the required results.

Simulator Concept and Classification

Simulator technology involves the use of computer-based models to simulate real-world scenarios and predict their outcomes. In the oil and gas industry, simulators can be used to predict well performance, optimize drilling operations, and improve workover operations. Simulators can be classified into three main categories: physical simulators, mathematical simulators, and hybrid simulators.

Simulator Design and Development

Simulators are built using specialized software and hardware to imitate real-world circumstances and scenarios. Simulators employ computer languages such as Python and MATLAB, as well as hardware such as sensors, actuators, and controllers.

Applications and Benefits of Simulators

Simulators are used in the oil and gas industry for a variety of purposes, including well performance prediction, drilling optimization, and workover planning and execution. The benefits of employing simulators include lower costs, higher safety, efficiency, and better decision-making.

Downhole Operation Simulator

Components of the System and Functional Features

DOS systems are made up of numerous parts, including software, hardware, and sensors. DOS systems employ software to model the downhole environment and the behavior of fluids and materials within the wellbore. Sensors that measure pressure, temperature, and other downhole characteristics, as well as controllers that regulate equipment performance, are utilized in DOS systems. Downhole operation simulators provide the ability to simulate various wellbore scenarios, optimize workover operations, and provide real-time input on downhole conditions.

Case Studies and Effect Evaluation

DOS technology has been employed in a variety of oil and gas sector applications, including work planning and execution, failure diagnosis and management, and work optimization and improvement. DOS technology has been proved to increase the efficiency and efficacy of workover operations while also lowering costs and improving safety.

Portable Workover Simulator

Applications of Downhole Operation Simulator in Oil and Gas Workover

Work Planning and Execution

DOS technology can be utilized to simulate multiple wellbore scenarios and optimize workover operations during workover planning and execution. Operators can detect possible issues and design more effective workover plans by mimicking the downhole environment. DOS technology can also be used to instruct workers on workover procedures and to improve their skills.

Failure Diagnosis and Handling

DOS technology can be utilized in failure diagnosis and handling to pinpoint the source of downhole problems and devise efficient solutions. Operators can discover the reason of a breakdown and develop a plan to rectify it by mimicking downhole circumstances. Furthermore, DOS technology can be used to monitor downhole conditions in real time and change equipment to alleviate problems as they emerge.

Work Optimization and Improvement

DOS technology can be used to optimize workover operations and improve well performance. By simulating different scenarios, operators can identify the most effective solutions to improve well productivity and extend the life of the well. Additionally, DOS technology can be used to monitor downhole conditions and make adjustments to equipment to optimize well performance.

Conclusion

Contributions and Research Findings

DOS technology has been proved through research to considerably improve the efficiency and efficacy of workover operations in the oil and gas industry. DOS technology has been proved to lower costs, increase safety, and boost worker productivity.

Limitations and deficiencies

One disadvantage of DOS technology is that it necessitates the use of professional staff who are familiar with the system’s software and hardware. Furthermore, DOS technology can be costly to adopt, particularly for smaller businesses.

Directions for Future Development and Research

Future DOS technology research should concentrate on improving system usability and lowering expenses. Furthermore, research should concentrate on the development of new uses for DOS technology, such as wellbore stimulation and enhanced oil recovery.

Key Points of High-pressure Homogenizer

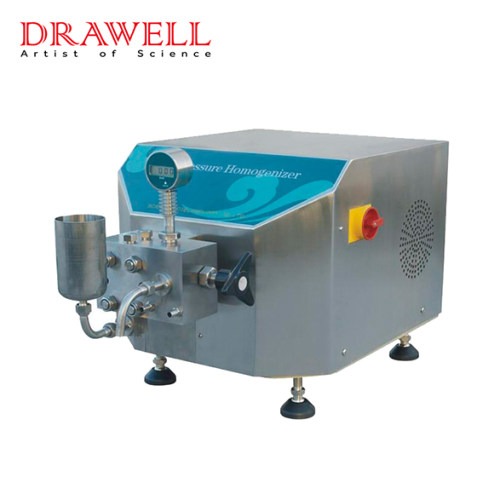
High-pressure homogenizer HPH is an online dispersion machine with excellent efficiency, energy savings, and continuous ultrafine emulsion generation. In contrast to other IKA in-line equipment, the HPH’s dispersing action is not based on the rotor/stator principle. Self-decompression of the liquid from up to 2000 bar to ambient pressure improves homogenization in the homogenizer.

Drawell high-pressure homogenizer HPH uses the same amount of energy as standard gear ring dispersers while producing more acceptable emulsions. High-pressure homogenizers are advised for disintegration down to the nanoscale; nevertheless, these homogenizers achieve lower flow rates than traditional dispersions.

High Pressure Homogenizer

How to Use a High Pressure Homogenizer?

1. Installation

Install the high-pressure homogenizer on a flat and sturdy desktop, then one by one install the high-pressure pump, homogenizer valve, pressure gauge, check valve, sample tank, and other components (each component is relatively independent and can be disassembled and installed independently).

Prepare an air compressor or nitrogen tank and circulate cooling water at the same time. The air compressor or nitrogen tank is used to supply the minimum pressure (5-10bar) required by the dynamic homogenization valve, as well as the pressure when the pipeline is flushed and the circulation cooling. When the sample is chilled, water is employed as a cold supply to guarantee that the sample maintains a low temperature during the homogenization process, avoiding sample denaturation and inactivation.

2. Cleaning and Disinfection

Before beginning the machine, inspect the complete sample path to confirm that the tubing is clean. Remove all components from the entire sample channel, then rinse with pure water, then 0.5M NaOH for a short period, and finally warm water.

After cleaning, each component can be sterilized with hot steam, and the pipeline can be sanitized for about 10 minutes after installation using a hot steam cycle.

3. Operation

Before starting the homogenizer, inspect the homogenized liquid to ensure that it is free of contaminants. Impurity particles, particularly metal particles, will harm the pipeline and the homogenizing valve, reducing the homogenizer’s service life.

Examine the high-pressure homogenizer’s pipeline to confirm that all components are correctly mounted and sealed, and that all bolts are securely fastened. Check the air supply (compressor or nitrogen tank, for example) to ensure that the needed pressure is available; Check the cooling water to ensure that the cooling circulation water was produced ahead of time in accordance with the process requirements, and that the cooling water pipeline was connected.

The small amount of liquid remaining in the pipeline is entirely drained before the HPH of the high-pressure homogenizer begins to work, and the sample is placed into the sample tank and pre-homogenized twice under air pressure.

Then, depending on the job needs, increase the homogenization pressure and begin homogenization. Following the completion of the homogenization, the pressure is decreased to zero and the substance liquid is discharged.

4. Maintenance

Immediately after homogenization, rinse with warm water and 0.5M NaOH in a cycle, followed by a rinse with clean water. It can be adequately aerated and pressured during this operation to speed up the cycle and rinse the pipeline more quickly and thoroughly. To finish the cleaning process, rinse 1-2 times with 50% alcohol.

Fill the sample tank and tubing with 70% alcohol solution for the next use after cleaning. If the entire pipeline needs to be sterilized, a hot steam cycle for around 10 minutes is used after the cleaning is finished.

Finally, switch off the power, turn off the air source and cooling water, and so on.

Precautions for Using High Pressure Homogenizer

1. Homogenizing pressure

The homogenization pressure of the high-pressure homogenizer is determined by the material and liquid properties. To minimize unexpected pressure changes, the pressure should be progressively increased during the process of increasing the pressure.

The material homogenization pressure should normally not exceed 2000bar during the homogenization process. To a certain extent, the high-pressure homogenizer allows for overload operation. For a limited period of time, the equipment can operate at 20% overpressure. The control box circuit will then immediately activate the cut-off protection mechanism, which will stop the machine from running. It can be turned back on and work after 30 seconds.

If the pressure cannot rise during the homogenization process, it means that the upper one-way valve is blocked, just use a thin iron wire to pass the ball valve.

2. What Should You Do If the Sample in the High-Pressure Homogenizer Has Air Bubbles?

A high-pressure homogenizer equipped with a dynamic homogenization valve enables the sample to contain air bubbles or to be emptied.

When the sample contains air bubbles or is empty, the homogenizing valve stem and valve seat will clash to some amount during the homogenization process, causing significant wear on the valve stem and valve seat, especially for the manually adjusted homogenizing valve, not only during the homogenization process but also thereafter. It is simple to wear down the homogenizing valve and even directly lead to its fragmentation, rendering it inoperable. Furthermore, it will generate a lot of noise during the homogenization process.

The dynamic homogenizer valve will reduce its damage and noise better, but it is generally recommended to avoid the long-term use of samples containing a large number of air bubbles and the occurrence of empty samples in the pipeline, which can effectively prolong the service life of the homogenizer valve.

Lab Blenders Stomacher

3. What Should You Do If Liquid Leaks From the High-Pressure Homogenizer?

There are no o-rings or gaskets in the high-pressure homogenizer’s whole sample route, and all face seals are precision-machined metal-to-metal or metal-to-ceramic seals that do not leak liquids.

However, if it is installed incorrectly, if the sample tank and one-way valve are not entirely buckled, or if a component is not properly installed after disassembly, liquid leakage will occur. At this point, all that remains is to inspect the pipeline and install each component appropriately in accordance with the installation manual’s specifications.

If the sample is poisonous and harmful, it will endanger and pollute the operating environment and operators. In this case, the above phenomenon can be avoided by simply tightening the sample tank and then flushing the sample passage with air and pressure.

What are the key points of Selecting Web Guide Systems for Different Types of Material

In manufacturing operations across various industries, web guide systems play a crucial role in ensuring precise alignment and material control. However, when it comes to selecting and implementing online directing systems, different types of materials require specific considerations. This article explores the applications and key factors to consider for web guiding systems in connection to various material types.

Applications of web guide system

Web Guide Systems for Paper and Printing Materials

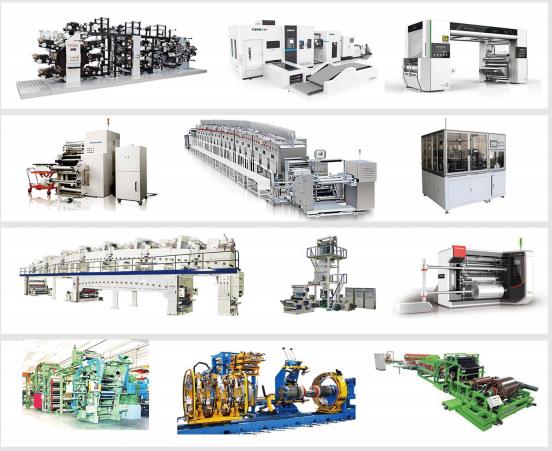
In the paper and printing industries, web guide systems are extensively used to maintain proper alignment and tension of paper and other printing materials. These systems are vital in achieving accurate registration, reducing waste, and enhancing overall print quality. When selecting web guide equipment for this application, factors such as the sensitivity of paper to tension fluctuations, web width, and the need for high-speed and precise registration control should be taken into account. Additionally, the web guide control system should be capable of accommodating different paper grades and sizes, as well as variations in coatings or finishes that may affect the surface characteristics of the material.

Web Guide Systems for Films and Flexible Packaging Materials

Web guide systems are critical in the flexible packaging industry to ensure proper film alignment during printing, laminating, and slitting operations. Films used in flexible packaging can vary in thickness, elasticity, and surface properties, posing unique challenges for web guiding. Elasticity, which affects the gripping and guiding mechanisms of the web guiding system, is particularly important in this application. Moreover, the system should maintain precise tension management to prevent film stretching or wrinkling during the guiding process.

Web Guide Systems for Nonwoven Materials

In nonwoven production, Web guide control systems are employed to align and manage materials such as spunbond, meltblown, and composite nonwovens. Nonwoven fabrics are often delicate and require sensitive handling and precise control to avoid damage or misalignment. Considerations for web guiding systems in this application include the delicate nature of nonwoven materials, the need to minimize contact to avoid distortion, and the ability to handle varying material widths and thicknesses.

web guide machine

Web Guide Systems for Metal Foils and Sheet Materials

Web guiding systems are used in sectors like metal processing and packaging to guide and control metal foils and sheet materials during manufacturing processes. Metal foils can be rigid, necessitating robust guiding mechanisms for proper alignment. In this application, web guide control systems must consider the stiffness and surface properties of metal foils, which may require specific guiding mechanisms and robust control systems. The system should provide precise tension management and be capable of handling variable material thicknesses and widths.

Web Guide Systems for Textiles and Fabrics

In textile manufacturing, web edge guide systems are employed to align and manage fabrics during weaving, printing, and finishing activities. Fabrics can vary in thickness, flexibility, and weave patterns, requiring adaptable guiding devices and accurate tension control. Web guide systems for textiles should incorporate flexible guiding parts to accommodate different fabric widths and patterns. Precise tension control is crucial to ensure proper alignment and prevent fabric distortion throughout the guiding process.

Web Guide Systems for Composite Materials

Web guide systems are utilized to maintain proper alignment during the layup operations involved in fabricating composite materials such as carbon fiber sheets or fiberglass laminates. Composite materials often require careful handling and precise alignment to maintain structural integrity. Special considerations for web guiding machines in this application include regulated tension, gentle handling, and low distortion during guiding. The system should deliver precise and customizable guidance to handle variable material widths and ensure proper alignment during the layup process.

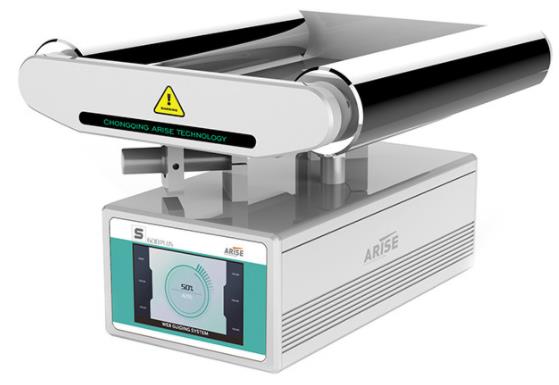
web guide system

Web Guide Systems for Adhesive Tapes and Labeling Materials

Web guide control systems are necessary in the production of adhesive tapes and labels to ensure perfect alignment and tension control. Accurate registration and consistent alignment are crucial for ensuring the quality and reliability of adhesive products. In this application, web guiding equipment must offer precise registration, minimize waste, and provide reliable edge detection for consistent guiding of narrow webs. The system should be capable of delivering precise guidance to handle varying web widths and maintain exact alignment throughout the manufacturing process.

Web Guide Systems for Foam and Foam-based Materials

In the foam material manufacturing industry, web guiding systems are employed to ensure perfect alignment and tension control during cutting, slitting, and laminating operations. Foam materials can be compressible, requiring specialized guiding systems capable of delicate handling. Compressibility and flexibility are important considerations for web alignment systems in this application. The system should provide precise and gentle web guiding to prevent material distortion or damage during the process.

Summary

Web guide systems are indispensable in industries dealing with various material types. Understanding the applications and unique considerations for each material type is crucial in selecting the appropriate web guiding machine. Carefully considering factors such as material properties, web width, tension control needs, and alignment precision is essential for achieving optimal performance and productivity in material handling and manufacturing operations. By choosing the right web guiding system for a specific material, industries can enhance quality, productivity, and overall production performance.

Why Heat Treatment is Imporant for Automotive Fasteners

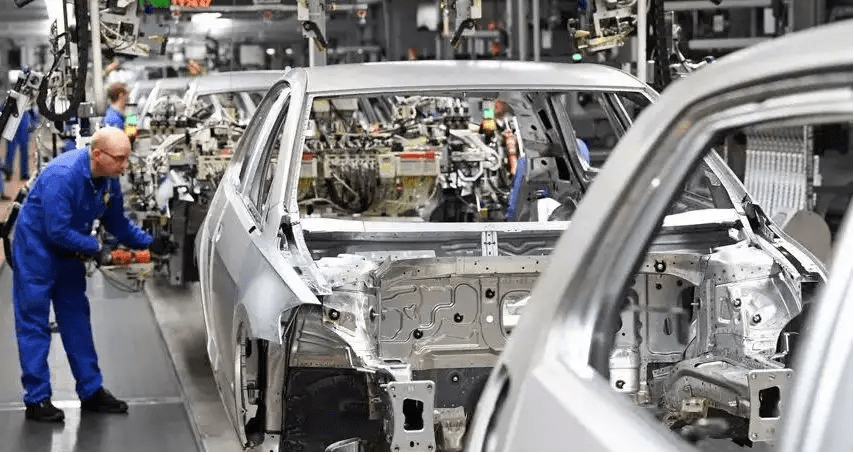
With the development of the automotive industry, the requirements for automotive fasteners have become higher and higher. The main kind of high-intensity automotive fasteners is bolts which all need to be treated with heat treatment to improve the comprehensive mechanical performance of the product and achieve the specified tensile strength. Heat treatment process technology is the key factor in the production of automotive fasteners.

automotive fastener

Factors affecting heat treatment process of automotive fasteners

Heat treatment equipment

The continuous mesh radiant-tube furnace is most widely used. It has the advantages of uniform heating, stable quality, good working environment, reducing collision of parts, less gas consumption, and small energy consumption.

According to the requirements of the process, dephosphorization function can be added on the cleaning equipment of production line, to remove the phosphorurative layer of the fastener surface before heating. For large size high-strength bolts, to prevent quenching distortion, the UNICASE series mult-purpose chamber furnace should be adopted to heat treatment process.

The heat treatment process of continuous mesh radiant-tube furnace production line: loading-cleaning-heating-quenching-cleaning-tempering-coloring-rolling out, can realize carbon potential control and automatically working.

Heat treatment raw material

The mostly automotive fastener is made of carbon and alloy steel. In addition to the high -intensity hexagonal bolt, according to the GB/T1231 requirements, the materials with specifications below m30 are specified, the other bolts are not clearly specified in international standards. It is only a guide to indicate the alloy elements to be added.

fastener manufacturer

Control methods of heat treatment process for automotive fasteners

The principle of heat treatment process

For the products with the same materials, when the size of the section is different, the quenching degree is different. Although the same quenching and tempering process is adopted, its mechanical properties are different. The larger the cross -section is, the worse the quenching ability is, and the worse the mechanical properties are. At the same time, the same raw materials allow their chemical composition to fluctuate within a certain range. Especially carbon steels will vary from steel mills as the different smelting technology and standards. The finished products produced by the same process must have performance differences.

The quenching heating temperature is mainly determined according to the chemical composition of the steel which is the main factor and the specific process. According to the different quenching medium, the quenching heating temperature is also different.

Due to the comprehensive effect of the organizational stress and thermal stress, the maximum tensile stress will be located near the surface of the parts, which may cause hardening crack. This size is related to the used quenching medium. For the bolts, the diameter of water quenching is 8-10mm and the diameter of oil quenching is 20-39mm. When the bolts in dangerous diameter are quenched, appropriate measures must be taken to prevent hardening crack.

Hydrogen relief treatment

The energy saving and lightweight development of automotive industry has high requirements for the engine design and dynamical system, which includes weight reduction and highly strengthened of bolts and nuts. But as the intensity increases, the fracture caused by hydrogen embrittlement has become a very prominent problem. During the heat treatment process, hydrogen relief treatment must be performed.

Tempered martensite is most sensitive to hydrogen embrittlement. Therefore, the heat treatment process can be adjusted to reduce the generation of Tempered martensite structure.

To prevent hydrogen embrittlement, the high -strength fastener under 1000-1300MPa must be done hydrogen relief treatment after the electroplating. During hydrogen removal, the fastener is heated to a certain temperature and maintains for a period of time and the hydrogen in the material will gather is to form hydrogen molecules. There are two main reasons for incomplete hydrogen removal. One is that there is no timely hydrogen removal, and the other is that the hydrogen removal time is too short.

Strengthen the measurement of fastener center structure

During the heat treatment process of automotive fasteners, as the effects of factors such as quenching heating temperature, quenching ability of materials, and quenching cooling speed will produce ferritic structure in the center of the fastener. Too much ferritic structure will reduce the hardness and strength of the bolt and affect the applications of fasteners. In actual production, For bolts with a large amount of ferrite in the center, when the hardness of the center structure is lower than the product requirements, the improvement of tensile strength is often adopted to control the quality of the product.

In order to control the heat treatment quality of the automotive bolt, it is necessary to measure the ferrite content in the center part of bolts, checking the hardness of the head or tail after quenching and tempering respectively.

heat treatment process

What should be paid attention to for heat treatment process of automotive fasteners

Adopting non annealing cold heading steel, non-quenched and non-tempered steel

In order to ensure the performance of cold forming for the automotive fastener, cold heading steel needs spheroidizing annealing in advance, adjusted through the chemical composition of the steel. During the rolling process, the rolling and cooling are controlled to reduce the deformation resistance in the process of cold forming.

Improving the technical documents of thermal treatment process

The heat treatment process is a special process that can’t ensure the quality of the product through subsequent inspections and testing. Therefore, it must have a reasonable system to achieve its control. First of all, identify the factors that may cause process failure, and do a good job of formulating heat treatment process technology. Secondly, establish a comprehensive heat treatment process management system with the documents which clearly indicates the operation methods, process parameters and inspection methods. At the same time, it should be particularly emphasized in the furnace loading method and the batch of furnace and test the raw materials and process conditions of fasteners before heating. It should adopt statistical technology to analyze, calculate and measure the heat treatment parameters, and look for the influence rules of heat treatment parameters on the product quality. Then adopt professional knowledge to continuously improve the heat treatment process technology.

Developing new heat treatment equipment

New heat treatment equipment should be developed to further improve the furnace temperature and carbon potential control technology, improving the cooling effect and cooling uniformity. It should be paid attention to the technologies of waste heat utilization, energy saving and emission reduction, which will reduce the production cost of heat treatment process.

Summary

Automotive fastener manufacturer should pay attention to the update of heat treatment equipment, selecting appropriate raw materials and continuously improve the heat treatment process system in production, strengthening dehydrogenation treatment, improving the quality of automotive fasteners.

在 WordPress.com 上免费创建您自己的网站。创建您自己的网站。
免费开始